If you’ve ever stood on a production floor making heat exchangers—whether for HVAC systems, automotive radiators, or industrial cooling units—you’ve probably seen a Fin Press Machine in action. These bulky, loud, unassuming machines turn thin aluminum or copper sheets into the tiny, precisely shaped fins that make heat exchangers work. But what most people don’t stop to ask is: why does temperature control matter so much for these fins? Last month, a customer of ours— a small, family-run radiator shop in Ohio—called us in a panic. They’d been running their old, unregulated fin press for years, but after a string of bad batches, their fins were cracking, their material was warping, and they were losing 15% of their raw aluminum stock each week. The problem wasn’t their operator, or the material, or even the machine itself. It was temperature control. That conversation stuck with me because I’ve spent the last 12 years selling and servicing Fin Press Machines, and too many operators write off temperature as a “set-it-and-forget-it” detail—until it breaks their production. Let’s break down what fin production temperature control actually is, why it’s non-negotiable, and how modern presses do it right. Fin Press Machine

First, let’s ground this in basics. A fin is not a flat sheet. It’s a series of thin, folded, often serrated blades designed to maximize surface area for heat transfer. To make one, you feed a continuous strip of aluminum (or sometimes copper) through a fin press, which uses a set of precision dies to stamp, bend, and cut the metal into that shape. The entire process happens at blinding speed—some presses run up to 120 strokes per minute, turning a 1000-foot roll of aluminum into finished fins in just a few hours. The metal, though, is a material that responds dramatically to heat. Room-temperature aluminum is hard and brittle enough that if you bend or stamp it cold, it will crack at the die lines. Too hot, and it will soften too much, stretching unevenly, warping into a wavy mess, or sticking to the die surfaces. That’s the core of temperature control in fin production: maintaining a narrow, consistent temperature range for the metal at the exact point it meets the dies, so every fin comes out identical, with no defects, and ready to be assembled into a heat exchanger.
Let’s get specific about the numbers here. For most aluminum fins, the ideal working temperature is between 180°F and 220°F (82°C to 104°C). That range isn’t arbitrary. At temperatures below 170°F, aluminum is in what’s called its “cold working” phase. Cold working is when you deform metal below its recrystallization temperature—for aluminum, that’s roughly 250°F. Stamping cold metal works fine for very simple shapes, but for the thin, intricate fins we need today—especially those with fine serrations or tight bend radii—cold stamping introduces micro-cracks that show up later when the fins are brazed. Brazing is the process of joining fins to tubes, and if there’s a crack in the fin, brazing material seeps in, blocks airflow, and ruins the heat exchanger’s efficiency. I’ve seen this first-hand: a customer in Michigan once blamed us for bad heat exchangers, only to find their old press was running at 150°F, and the cold-stamped fins had developed cracks that only expanded during brazing. We replaced their temperature control unit, and their defect rate dropped to under 0.5%. Go above 230°F, and you enter the “hot working” phase. Aluminum’s tensile strength drops sharply here—stamping it will cause uneven stretching, leading to fins that are too thin in some spots and too thick in others. Worse, when hot metal touches the dies, it starts to gall—sticking to the die surface, tearing bits of metal off every stroke, and leaving a rough, unusable edge on the fin. That’s another hidden cost: if metal galling builds up, you have to stop production every hour to clean the dies, costing time and risking human error from repeated stops.
Now, how do Fin Press Machines actually control this temperature? There are three primary methods, and I’ve seen good machines use all three in tandem, not just one. The first and most common is die heating. The stamping dies—those hardened steel plates that shape the fin—are equipped with embedded cartridge heaters, or sometimes circulating hot oil lines, that warm the die surface. The die is the interface between the machine and the metal strip, so if the die is at the right temperature, it transfers consistent heat to the metal as it’s pressed. But here’s the thing: temperature control for dies isn’t just cranking up the heat. Good presses use thermocouples placed directly on the die surface, not just inside the housing, to measure real-time temperature, and PID (Proportional-Integral-Derivative) controllers to adjust heat output dynamically. A cheap alternative is a thermostat that turns the heater on and off at set intervals, which causes temperature swings of 20 or 30 degrees per minute—exactly what ruined that Ohio customer’s old press. Our machines use PID controllers with 0.5°F accuracy, so the die stays within 1 degree of the target temperature, even when running at full speed.
The second method is strip preheating. For high-volume production, the raw aluminum strip is fed into the press at room temperature, so it cools the die slightly every time it passes through. Preheating the strip means it enters the press at the right temperature, so the die doesn’t have to compensate for cold metal, and the combination of preheat and die heat keeps the metal at the ideal working range. Preheating is usually done with infrared heaters mounted just before the die station, or with induction heating that targets the exact width of the metal strip. This is particularly important for copper fins, which have a higher thermal conductivity—they lose heat faster to the die, so without preheating, you’d have to crank the die heat so high that the die itself wears out prematurely. I remember a customer who switched from aluminum to copper fins for a line of commercial HVAC units, and initially skipped strip preheating. Their die life dropped by 40%, and their fin defect rate hit 22% until we added the preheater. It’s a small investment that pays for itself in three months, easy.
The third, and often overlooked, part of temperature control is cooling. Wait—cooling? If we’re heating, why would we need cooling? Because some fin designs require faster cooling after stamping, to set the shape before the strip moves on to the next station (like cutting or perforating). Also, if the press runs for hours, the motor and hydraulic components generate extra heat that can transfer to the dies and strip, throwing off the temperature balance. Good presses have closed-loop cooling systems for the die and the machine’s internal components, so if the temperature rises too high, it kicks in immediately, keeping the whole system stable. I’ve had operators tell me their “temperature control” is just turning off the heater when it gets too hot, but that’s reactive, not proactive. Modern systems anticipate changes—like a roll of aluminum that’s slightly colder than the last one, or a spike in production speed—and adjust heating and cooling before the temperature drifts.
Now, let’s talk about common mistakes I see operators make, because this isn’t just about machine specs—it’s about how you use it. The first mistake is assuming temperature is a set-it-and-forget-it value. I once had a customer who set their dies to 200°F in the morning, then left it all day, not realizing that as the die wore down, its heat distribution changed, so some spots were 250°F and others were 160°F. They only checked the temperature at the start of the shift. Big mistake. Our machines have alarms that notify operators if temperature deviates more than 2°F, and a log that shows you temperature over time, so you can spot trends instead of reacting to bad fins. Another mistake is mixing materials. If you switch from 0.1mm aluminum to 0.15mm aluminum, or from a 3000-series alloy to 5000-series, the ideal temperature changes too. Thicker metal needs a slightly lower temperature (it has more thermal mass, so it heats up slower), while harder alloys need a bit more heat to prevent cracking. Operators who use the same temperature for every material will have defects, no matter how good the machine is. The third mistake is neglecting maintenance. Thermocouples get dirty, cartridge heaters wear out, cooling lines get clogged with scale. A thermocouple that’s covered in aluminum shavings will give a false temperature reading, making the controller think the die is 200°F when it’s actually 150°F. We recommend checking thermocouples monthly, calibrating the temperature system every three months, and replacing heaters before they fail—something that’s easy to do during a routine service, not when a production line is down for 8 hours because the die suddenly went cold.
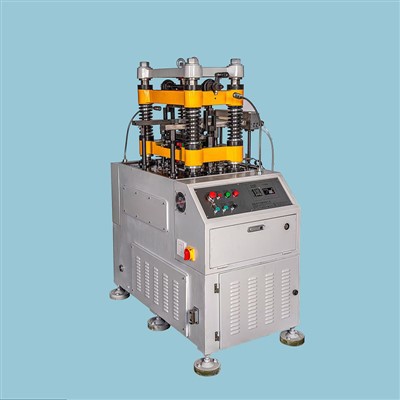
So, what does this mean for you, if you’re in the market for a Fin Press Machine? Temperature control isn’t a feature—it’s a core component that directly affects your yield, your material costs, your downtime, and the quality of your final product. A press with a cheap, on-off thermostat and no preheating or cooling system might cost $10,000 less upfront, but if your defect rate is 10% vs. 0.5% with a machine that has precise temperature control, you’ll lose that $10,000 in raw material in less than two months. Add in the cost of downtime for cleaning dies, fixing cracked fins, and reworking bad parts, and the gap only gets wider. Our team has worked with hundreds of production facilities, from small local shops to large OEMs, and we’ve seen time and time again that the best fin presses aren’t the fastest ones—they’re the ones that keep temperature consistent, no matter how long they run, no matter what material you feed them. If you’re struggling with fin defects, high material waste, or frequent die replacement, temperature control is almost certainly the root of the problem. We offer free on-site assessments, where our technicians will walk your production floor, test your current press’s temperature system, and show you exactly how much you’re losing each week to bad temperature control. No pushy sales pitches, no hidden fees—just real data from real production lines. If you’re ready to cut your defect rate, lower your material costs, and get more consistent, high-quality fins, we’d be happy to connect and talk through your needs.
Fin Forming Machine Reference
ASM International. (2008). Metals Handbook: Volume 4, Heat Treating. ASM International.
Dieter, G. E. (1986). Mechanical Metallurgy (2nd ed.). McGraw-Hill.
Finishing Industries Association. (2021). Guide to Heat Exchanger Component Manufacturing. Finishing Industries Association.
Suichang Lvye Machinery Co., Ltd.
We are one of the most professional fin press machine manufacturers in China, also support customized service with low price. We warmly welcome you to buy discount fin press machine for sale here from our factory. If you have any enquiry about quotation, please feel free to email us.
Address: No. 402, Mudanting East Road, Miaogao Street, Suichang County, Lishui City, Zhejiang Province
E-mail: L528753@outlook.com
WebSite: https://www.suichanglvye.com/
