If you’ve ever stood next to a plansifter running in a flour mill, grain processing plant, or feed manufacturing facility, you know that that steady, rhythmic vibration isn’t just background noise—it’s what separates fine flour from middlings, semolina from bran, and makes the entire process run efficiently. As someone who’s supplied plansifters to operators across North America and Europe for over a decade, I can say with certainty that adjusting the vibration amplitude of your plansifter is one of the most critical (and most often overlooked) tasks for maintaining consistent separation, reducing wear on your machine, and avoiding unplanned downtime. Too many operators either run the vibration too high (blowing product out of the sieve frames, wasting raw material and damaging mesh) or too low (leaving product stuck in layers, slowing throughput and lowering final product quality). Today, I’m walking you through exactly how to adjust that amplitude safely, effectively, and with the same practical, on-the-floor knowledge I’ve built working alongside the teams that use our plansifters every day. Plansifter
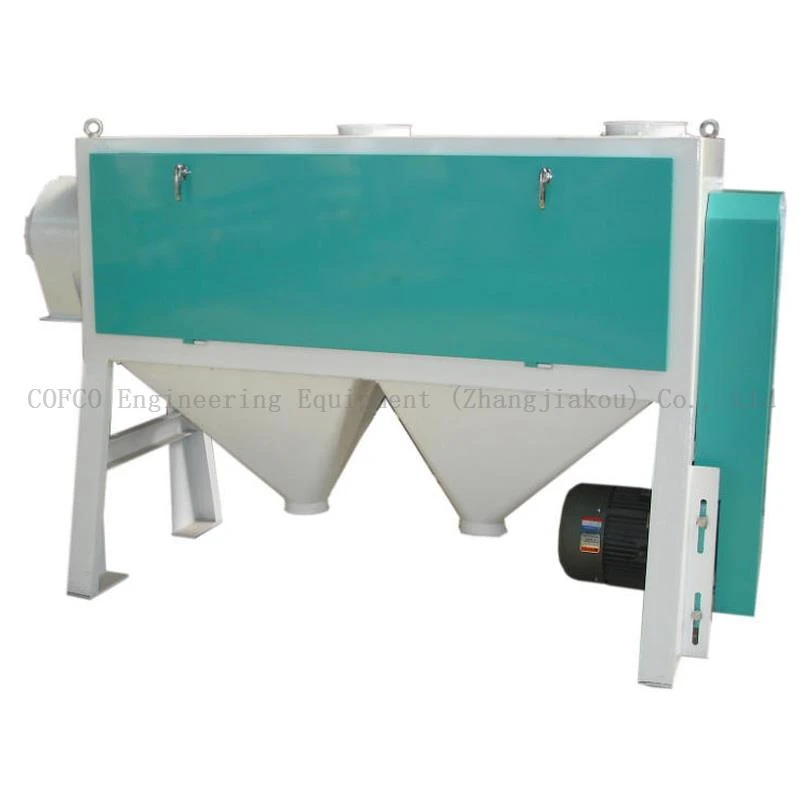
First, let’s get clear on what vibration amplitude in a plansifter actually is, because there’s a lot of misinformation out there. Amplitude refers to the distance a plansifter’s vibrating base (and the entire sieve box mounted on it) moves back and forth in a single cycle. It’s measured in millimeters, and for standard grain and flour plansifters, the ideal range is almost always between 2mm and 5mm—depending on the type of product you’re processing, the mesh size of your sieves, and the number of layers in your machine. Too small, and the product doesn’t fluidize; it clumps, sits still, and can’t move through the sieve apertures. Too large, and the product gets thrown too forcefully, landing outside the designated collection trays, or the sieve cloth stretches and tears prematurely, or the plansifter’s structural parts (the base, the hangers, the drive shafts) take extra stress that leads to breakdowns.
Before we jump into adjustments, let’s talk about a critical first step: confirming why your amplitude is off. I can’t tell you how many times I’ve arrived at a mill to help with a performance issue, only to find the operator tried to crank up vibration because throughput was low, when the real problem was they’d put a mesh that was too fine for semolina separation. Or worse, they adjusted the vibration without turning off the machine first, leading to a near-miss. So step zero: always lock out/tag out the power to your plansifter before doing any adjustments. No exceptions. Even if you think the machine is off, the drive shaft or counterweights can still move, and that’s a serious safety risk.
Next, locate the components that control amplitude on your plansifter. Every brand is a little different, but the core adjustment parts are the counterweights mounted on the main drive shaft. Plansifters use two sets of counterweights: fixed weights and adjustable weights. Fixed weights are usually bolted securely in place to set the baseline force, while adjustable weights are the ones you move to fine-tune amplitude. Some newer, larger models also have hydraulic or mechanical amplitude adjustment knobs, but 90% of the field units I service still rely on adjustable counterweights. You’ll find these counterweights inside a protective cover on the side of the plansifter’s drive housing—always make sure that cover is secured back in place after any work to keep dust and debris out, which can cause drive failure.
Once you’ve confirmed safety and located your counterweights, it’s time to make the adjustment. Let’s break this down into a simple, repeatable process that works for most standard operations:
- Start at the lowest setting. If you’re setting up a new plansifter, or switching to a completely different product (say, moving from all-purpose flour to whole grain semolina), start with the adjustable counterweights set all the way in, so their mass is closest to the center of the drive shaft. This gives you the smallest possible amplitude.
- Run a test batch. With the power restored (and lockout/tag out removed), run your standard product at your normal production speed for 10 to 15 minutes. Don’t change anything else during this test—same feed rate, same sieve layers, same moisture content in the grain. This is the only way to get an accurate reading of how your current amplitude is performing.
- Evaluate the results. Watch three key areas: the sieve cloth, the product flow, and the collection trays. If the product is sitting in clumps on the sieves, moving too slowly, and only partially separating into fractions, your amplitude is too low. If the product is being thrown over the edges of the sieve frames, or you’re finding fine flour in your coarse middlings tray, amplitude is too high. You want to see consistent, even fluidization of the product—like a gently moving fluid—with each layer moving at a steady speed, and all fractions landing exactly in their designated collection bins.
- Make small adjustments, one weight at a time. If you need more amplitude, move one adjustable counterweight one bolt hole outward (away from the center of the drive shaft). If you need less, move one inward. Always adjust both counterweights on the same side of the shaft equally—you can’t adjust only one, because that would cause uneven vibration, leading to the plansifter tilting, which ruins separation and puts extra stress on the hanger cables or springs. A quarter-inch movement on each weight is usually enough to change amplitude by 0.2mm, so don’t overdo it.
- Retest and repeat. After each adjustment, run another 10-minute test batch, recheck the flow and separation, and adjust as needed until you hit that sweet spot.
Now, there are a few product-specific nuances that I’ve learned over years of working with different operations, and these make a huge difference. For example, fine, low-moisture flour (all-purpose cake flour, pastry flour) needs a lower amplitude—usually between 2.2mm and 2.8mm. Too much amplitude here will blow the fine flour out of the sieves, leading to product loss and dusty work areas, and even worse, that fine flour can get caught in the plansifter’s drive parts, causing clogs over time. On the other end, coarse products like durum semolina or whole grain middlings need higher amplitude, usually between 3.5mm and 5mm, to help the larger particles move through the sieve apertures efficiently. If you try to run semolina at the same amplitude as pastry flour, you’ll end up with low throughput and coarse product that still has fine flour mixed in, because the particles aren’t moving enough to separate.
Another common issue I see is plansifters that have been running for years without any maintenance, leading to worn parts that throw amplitude off entirely. It’s not always the counterweights! Hanger springs that have stretched over time, or sieve frames that have become warped from repeated heating and cooling (common in facilities that use heat to dry grain), can change the effective amplitude even if you adjust the counterweights. I always recommend operators check these parts at least every six months: make sure hanger springs are the same length, no cracks or rust on the spring hooks, and sieve frames sit evenly on the base, with no gaps between the frame and the rubber gaskets. If you skip this, no amount of counterweight adjustment will get your plansifter running consistently.
I also want to address a mistake that new operators often make: adjusting amplitude on the fly during production runs to fix temporary issues. If you notice that a particular sieve layer is performing poorly one day, don’t crank up the overall plansifter amplitude to compensate—this will mess up every other layer. Instead, adjust the feed rate to that layer, or check if the sieve mesh is clogged (that’s a way more common issue than overall amplitude change). A clogged sieve will have uneven product flow, which looks like a vibration problem, but it’s actually a mesh issue. Clean or replace the sieve, and your flow will return to normal without touching the counterweights.
Now, for our customers and anyone looking to optimize their plansifter performance: if you’re unsure about your current amplitude setting, or you’ve tried adjusting counterweights and still aren’t getting the separation you need, we offer on-site performance checks and adjustment services that our team of experienced technicians will come to your facility, lock out/tag out safely, test your current amplitude, adjust counterweights or worn parts, and train your operators on how to maintain that setting moving forward. We’ve worked with mills of all sizes, from small local grain processors to large national feed manufacturers, and we know that every operation is different—there’s no one-size-fits-all setting, which is why we tailor our adjustments to your specific product, sieve layers, and production goals.
I’ll also note that regular maintenance checks can help you avoid most amplitude-related issues before they become problems. A quick weekly check of the counterweights (to make sure they haven’t worked loose from vibration), a monthly inspection of hanger springs and sieve frames, and a quarterly amplitude test will keep your plansifter running at peak efficiency, reduce downtime, and extend the lifespan of your machine parts. We include a maintenance and adjustment guide with every plansifter we supply, and our customer support team is always available to answer questions, no matter how small, or walk you through an adjustment over the phone if you’re in a pinch.
To wrap this up, adjusting plansifter vibration amplitude isn’t a complicated task, but it does require patience, attention to detail, and understanding of how your specific product interacts with the machine. Always start with safety, confirm that underlying parts aren’t worn before adjusting counterweights, make small increments, and test after every change. If you’re new to working with plansifters, or you’re dealing with persistent performance issues that adjustment alone hasn’t fixed, don’t hesitate to reach out to our team to discuss your needs. We don’t just supply plansifters—we partner with our customers to make sure their equipment runs as reliably and efficiently as possible, because when your plansifter works well, your whole operation works well.
Now, for anyone looking to upgrade their plansifter or optimize their current setup, contact our team to discuss your requirements and learn how we can support your operation. We look forward to helping you get the most out of your grain processing equipment.
Flour Automatic Packing Machine References
American Society of Agricultural and Biological Engineers. Vibration and Operation of Grain Processing Equipment. Standard ASABE S566, 2021.
Grain Processing Society. Plansifter Design, Operation, and Maintenance for Small to Mid-Sized Operations. 3rd Edition, 2019.
Miller, John. Optimizing Vibration Parameters in Plansifters for Wheat and Corn Separation. Journal of Grain Science and Technology, vol. 12, no. 2, 2020, pp. 45-52.
COFCO Engineering Equipment (Zhangjiakou) Co., Ltd.
As one of the most professional plansifter manufacturers and suppliers in China, we also support customized service. Please feel free to wholesale advanced plansifter for sale here from our factory. Quality products and reasonable price are available.
Address: No.4 ZhongLiang Street, high-tech industrial development zone, Zhangjiakou, Hebei, PRC
E-mail: mayihui@cofco.com
WebSite: https://www.ceeflourmill.com/
