When I first started out as a horizontal surface grinder supplier 12 years ago, I’d bring a beat-up old grinder manual to every shop floor walkthrough. The operators would crowd around, squinting at the dusty diagrams, and half of them would ask the same question: “How does this thing actually make metal flat enough to feel like glass?” Back then, I’d stumble through the explanation, mixing in tips from my grandfather who taught me the trade, and by the end, half the room would still look confused. These days, after selling nearly 400 horizontal surface grinders to job shops, aerospace part manufacturers, and mold makers across the Midwest, I can answer that question without pulling a single cheat sheet—and break it down in terms that even a new apprentice can follow. Let’s cut through the jargon and talk about how a horizontal surface grinder works, straight from someone who builds, repairs, and sells these machines for a living. Horizontal Surface Grinder
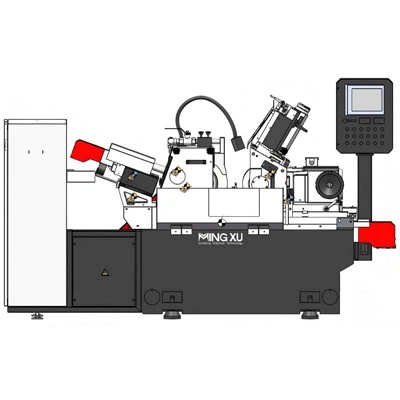
First, let’s get one basic fact straight: the “horizontal” part isn’t just a marketing term. It refers to the orientation of the grinding wheel’s spindle, the core part that does all the cutting. Unlike a vertical grinder, where the wheel spins straight down toward the work table, a horizontal grinder’s spindle lies parallel to the work table. That means the wheel spins around a horizontal axis, like a ceiling fan flipped on its side and mounted above the table. This design isn’t random—it’s the reason horizontal grinders produce consistent, flat surfaces faster than almost any other grinding machine on the market.
Let’s walk through the machine from the bottom up, starting with the work table, because that’s where the part you’re grinding spends most of its time. The table sits on two precision ways, usually made of hardened steel coated in a low-friction material like Turcite, so it slides back and forth smoothly with almost zero play. There are two main table movements: the cross feed and the longitudinal feed. Longitudinal feed is the back-and-forth motion, moving the part straight toward and away from the grinding wheel. Cross feed is the side-to-side motion, moving the part perpendicular to the wheel’s axis, like combing hair in overlapping strokes.
Now, how does the part stay still on the table while grinding? That’s where the chuck comes in. Most horizontal surface grinders use a magnetic chuck—powerful electromagnets that turn on when you flip a switch, clamping ferrous parts tight to the table. I always tell customers: if you’re grinding aluminum or brass, you’ll need a mechanical vise or a vacuum chuck, but 90% of the jobs we get are on steel, so the magnetic chuck is the workhorse. I’ve seen shops cut corners here by skipping the demagnetization step after grinding, which leaves tiny magnetic particles stuck in the part—great for scrap magnets, bad for precision parts that need to fit into a larger assembly. More on that later.
Next, the star of the show: the grinding wheel. This isn’t the flimsy wheel you use to sharpen a lawnmower blade. Horizontal surface grinder wheels are custom-made from abrasive grains, usually aluminum oxide for steel parts or silicon carbide for brass and aluminum, bonded together with a material like resin, vitrified clay, or rubber. The type of bond determines how the wheel behaves: vitrified bonds are hard, hold their shape well, and are great for heavy stock removal, while resin bonds are more flexible, perfect for finishing smooth, delicate surfaces. The key here is that the wheel has thousands of tiny, sharp abrasive points sticking out of its surface—each one is like a tiny cutting edge, designed to chip away micro-thin layers of metal. No, it doesn’t “smooth” the metal like sandpaper—it cuts, one tiny chip at a time.
The spindle that spins the wheel is mounted on a saddle, which moves up and down to adjust how deep the wheel cuts. That vertical movement is called the infeed, and it’s where precision really matters. On a good horizontal surface grinder, you can adjust the infeed in increments as small as 0.0001 inches—about the thickness of a human hair. That’s the difference between a part that’s flat to within a thousandth of an inch (the standard for most job shop work) and a part that’s off by enough to get rejected by a quality control team.
Now, let’s put it all together in a real working job, because that’s when the magic happens. Let’s say you’re grinding a set of steel mold plates, each 12 inches long, 6 inches wide, and 1 inch thick, and you need the top surface to be perfectly flat and within 0.0005 inches of thickness across the whole plate. Here’s what happens step by step:
First, the operator cleans the chuck with a rag and a little solvent to make sure there’s no dirt or metal shavings between the part and the chuck—those tiny bits would leave tiny dips in the ground surface, and you’d be redoing the job. They set the mold plate on the chuck, flip the magnetic switch, and give it a little tap with a rubber mallet to make sure it’s securely clamped.
Next, they dress the grinding wheel. Dressing is a step I can’t stress enough, especially for new operators. As the wheel spins, the abrasive grains get dull and get clogged with tiny metal chips from the part—this is called glazing, and it makes the wheel stop cutting smoothly, leaving a rough surface. To fix that, they run a diamond dresser (a small tool with hard, diamond-tipped points) against the spinning wheel, knocking off the dull grains and opening up new sharp ones. Dressing also ensures the wheel’s surface is perfectly round and aligned with the table, which is why a poorly dressed wheel will never produce a flat part, no matter how good the grinder is.
Now, the operator sets up the feeds. They set the longitudinal feed speed, usually between 20 and 100 feet per minute, depending on how much metal they need to remove. For roughing cuts, they might take a 0.005-inch infeed per pass, removing a thick layer of metal quickly. For finishing cuts, they drop that to 0.0005 inches, taking a tiny, almost invisible layer to get the surface smooth and flat. The cross feed is set to about half the width of the wheel, so each stroke overlaps the last, leaving no gaps in the ground surface.
As the machine runs, the wheel spins at 1,500 to 3,600 RPM, moving back and forth across the mold plate, cutting tiny chips of metal. The coolant system—another critical part most first-timers forget about—sprays a steady stream of water-based coolant onto the wheel and part. Why? First, it cools down the cutting edge of the wheel: grinding creates a lot of friction, and if the wheel gets too hot, it can warp, burn the metal, or even crack. Second, it flushes away the tiny metal chips, keeping the wheel from glazing and leaving those chips from scratching the finished surface. I had a customer last year who saved $15,000 a year in scrap just by upgrading his coolant system on an older grinder—small detail, big impact.
Once the roughing cuts are done, the operator cleans the chuck again, runs the part through a demagnetizer to remove any leftover magnetism, and checks the thickness with a micrometer. Then they crank the infeed down for the finishing cuts, usually two or three light passes, until the part is within spec. After the final pass, they demagnetize the part one more time, clean it, and it’s ready to go to the next step in production.
Wait a second—what makes a horizontal surface grinder better than, say, a vertical grinder? Let’s answer that, because it’s a common question I get. Horizontal grinders have a larger contact area between the wheel and the part, which means they can remove more metal faster and produce flatter, more consistent surfaces than vertical models, which are better for smaller, more detailed work. For jobs that need flatness and large areas—like mold plates, machine tool beds, or engine blocks—you won’t beat a horizontal surface grinder.
But like any machine, how well it works depends on setup and maintenance. I tell all my customers that a horizontal surface grinder is only as good as the way you care for it. Lubricate the ways every month, check the alignment of the wheel and chuck every quarter, dress the wheel before every job (don’t skip that step!). I’ve seen a $50,000 grinder turn into a $10,000 paperweight because the owner forgot to clean the ways and let rust build up—rust ruins the precision of the slide, and once that’s gone, no adjustment will bring it back.
Now, let’s talk about why this matters, beyond just shop floor jargon. Parts made on horizontal surface grinders are everywhere: the mold that makes your phone case, the engine block in your car, the blades on a wind turbine, even the parts that go into medical devices like pacemakers. If a mold plate is off by a thousandth of an inch, the plastic part it makes won’t fit right, and you have to scrap thousands of units. That’s why precision in grinding isn’t just about making a part look good—it’s about making products that work.
As someone who’s been selling horizontal surface grinders for over a decade, I’ve learned that most people don’t care about the science behind the machine until their parts get rejected. They just want a machine that runs smoothly, makes flat parts, and doesn’t break down when they have a tight deadline. That’s why I don’t just sell grinders—I work with operators and quality teams to make sure they get the right machine for their jobs, and teach them how to use it correctly. Whether you’re a small job shop grinding parts for local contractors or a large aerospace manufacturer needing to meet strict ISO standards, there’s a horizontal surface grinder that fits your needs.
If you’re looking to upgrade your current grinding setup, or you’re ready to buy your first horizontal surface grinder, I’m here to help. We work with shops of all sizes, from start-ups to Fortune 500 facilities, and can walk you through the process of picking the right model, setting it up, and training your team. No pushy sales pitches, no hidden fees—just honest advice from someone who’s been in the shop working next to the machines for years. Reach out to connect, and let’s talk about how a horizontal surface grinder can make your parts better and your production more efficient.
Precision Centerless Grinder References:
- Todd, R. H., Allen, D. K., & Alting, L. (1994). Manufacturing Processes Reference Guide. Industrial Press Inc.
- Kalpakjian, S., & Schmid, S. R. (2014). Manufacturing Engineering and Technology (7th ed.). Pearson.
- Shaw, M. C. (1996). Metal Cutting Principles. Oxford University Press.
- American Society of Mechanical Engineers. (2018). B5.57-2018: Horizontal Surface Grinders. ASME International.
- WorkGrind Magazine. (2022). “Key Maintenance Practices for Precision Surface Grinders.” Industry Insights.
Wuxi Mingxu Machinery Equipment Co., Ltd.
As one of the most professional horizontal surface grinder manufacturers and suppliers in China, we’re featured by quality products and good price. Please rest assured to buy the best horizontal surface grinder for sale here from our factory. Also, custom service is available.
Address: No. 5-5 Jinke Wealth Plaza, Changjiang North Road, Xinwu District, Wuxi City, Jiangsu Province
E-mail: yingyingmxjd@163.com
WebSite: https://www.mingxu-china.com/
